
Water soluble film is used across a growing range of industries, including packaging, agriculture, cleaning products, healthcare, and industrial applications. As demand increases, businesses need to carefully evaluate suppliers to ensure the film meets their specific performance, safety, and production requirements.
When comparing Water Soluble Film Manufacturers, it is important to look beyond product availability and consider factors such as material quality, technical capabilities, customization options, production consistency, and compliance with applicable standards. A reliable manufacturer should be able to provide clear information about its materials and manufacturing processes.
Understand the Film Material and Its Properties
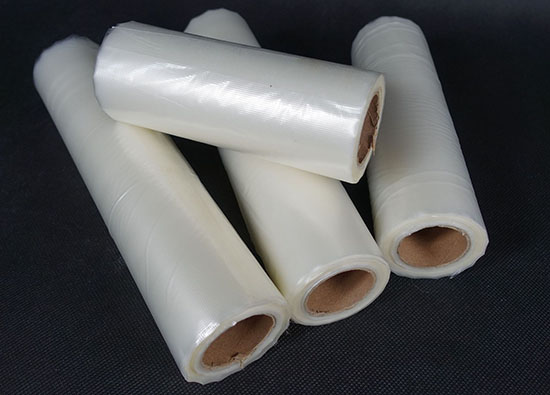
The first consideration is the type of water soluble film being offered. Polyvinyl alcohol, commonly known as PVA or PVOH, is widely used because it can dissolve in water while providing useful film-forming properties.
Different formulations can have different dissolution temperatures, tensile strength, flexibility, thickness, and moisture resistance. These characteristics should match the intended application rather than being selected solely based on price.
Evaluate Manufacturing Quality
Consistent manufacturing is essential when water soluble film is used in automated packaging or high-volume production. Variations in thickness, strength, or dissolution behavior can affect both product performance and processing efficiency.
When evaluating a supplier, consider whether it has established quality-control procedures covering raw materials, film production, thickness, physical properties, and finished products. Consistent testing can help reduce unexpected variations between batches.
Production Capacity and Stability
Manufacturing capacity is another important factor, particularly for companies that expect demand to increase. A supplier should have sufficient production resources to maintain consistent delivery without compromising quality.
It is also useful to ask about production lead times, minimum order quantities, inventory practices, and the manufacturer’s ability to support long-term supply requirements.
Check Customization Capabilities
Water soluble film is not necessarily a one-size-fits-all material. Different applications may require specific film thicknesses, dimensions, dissolution characteristics, colors, or mechanical properties.
A manufacturer with appropriate technical capabilities should be able to discuss these requirements and determine whether an existing film grade is suitable or whether customization may be necessary.
Consider Application-Specific Performance
The right film should be selected according to how it will be used. For example, film designed for detergent packaging may have different requirements from film used for agricultural chemicals or industrial packaging.
Important factors can include:
- Dissolution speed and temperature
- Tensile strength and elongation
- Film thickness
- Moisture sensitivity
- Sealing performance
- Storage stability
- Compatibility with the packaged material
Understanding these characteristics before purchasing can help prevent problems during filling, packaging, transportation, and end use.
Review Testing and Quality Documentation
Reliable manufacturers should be able to provide appropriate technical documentation for their products. Depending on the application and market, this may include technical data sheets, test reports, specifications, and relevant compliance documentation.
Businesses should also clarify how products are tested and whether quality standards are applied consistently throughout production. Transparent documentation makes it easier to compare suppliers using objective criteria.
Examine Technical Support
Technical support can be particularly important when water soluble film is being integrated into an existing packaging process. Film behavior may be influenced by machinery settings, temperature, humidity, sealing conditions, and the characteristics of the packaged product.
A manufacturer that can provide practical technical information can help customers identify suitable film specifications and address compatibility issues during implementation.
Assess Packaging and Storage Requirements
Because water soluble film interacts with moisture, storage conditions deserve careful consideration. Excessive humidity or unsuitable packaging can affect film performance before it reaches the production line.
Ask manufacturers about recommended storage temperature, humidity levels, packaging methods, shelf life, and handling procedures. These details can help maintain material quality throughout transportation and storage.
Compare Overall Value Rather Than Price Alone
Price is an important purchasing consideration, but it should not be the only factor. A lower-cost film may become more expensive if inconsistent quality leads to packaging failures, production downtime, material waste, or additional testing.
A more useful comparison considers the complete value offered by each supplier, including product consistency, technical support, customization, delivery reliability, and long-term suitability.
Questions to Ask Before Selecting a Manufacturer
Before making a final decision, businesses can ask potential suppliers:
- What type of PVA or PVOH film is available for the intended application?
- What thicknesses and specifications can be produced?
- How is film quality tested during production?
- Can the film be customized for specific packaging requirements?
- What are the recommended storage conditions?
- What technical documentation is available?
- What are the typical production and delivery lead times?
- Can the manufacturer support larger volumes as demand grows?
The answers can provide a clearer picture of whether a supplier is equipped to meet both current and future requirements.
Final Considerations
Choosing a water soluble film supplier requires more than comparing product prices or specifications. Material performance, manufacturing consistency, customization, quality control, technical support, documentation, and supply reliability can all influence the success of the final application.
By evaluating these factors systematically, businesses can identify a manufacturer whose capabilities align with their technical requirements and production goals. This approach can also reduce supply risks and make it easier to maintain consistent product quality over the long term.